Mineral concentrate is one of the most valuable and most chemically aggressive bulk materials a site will ever store. Get the containment, drainage, and handling interface right and the stockpile becomes a controlled asset; get it wrong and you inherit acid runoff, corroded steelwork, and inventory losses that compound for decades.

Key engineering takeaway: A copper concentrate pile standing 10 m high at a bulk density of 2.0 t/m³ imposes roughly 200 kPa (about 20 t/m²) of vertical surcharge on the ground beneath it. That single figure drives foundation type, slab thickness, liner selection, and the entire capital cost curve of a concentrate Dust Explosion Prevention in Grain Storage Facilities: En... project. Design the pile geometry before you design the building — never the reverse.
Mineral Concentrate Storage Explained: Why Containment Design Drives Project Economics
Concentrates are the intermediate product of mineral processing: finely ground sulfide or oxide ore that has been upgraded by flotation or gravity separation to a saleable grade, typically between 20% and 30% copper, 50% to 60% zinc, or 45% to 70% iron. Particle size usually runs 80% passing 50–150 µm, moisture sits between 6% and 12% after filtration, and the material behaves somewhere between damp sand and a mildly cohesive powder.
What makes concentrate storage fundamentally different from grain or aggregate storage is not the physical handling — it is the chemistry. Sulfide concentrates oxidize in the presence of oxygen and water, generating sulfuric acid and heat. That means every storage decision carries a chemical consequence: the liner must resist low-pH leachate, the steel must resist acid attack, the ventilation strategy must manage sulfur dioxide and hydrogen sulfide, and the pile geometry must limit self-heating. Containment design is therefore not an environmental afterthought bolted onto a materials handling project — it is the primary cost and risk driver.
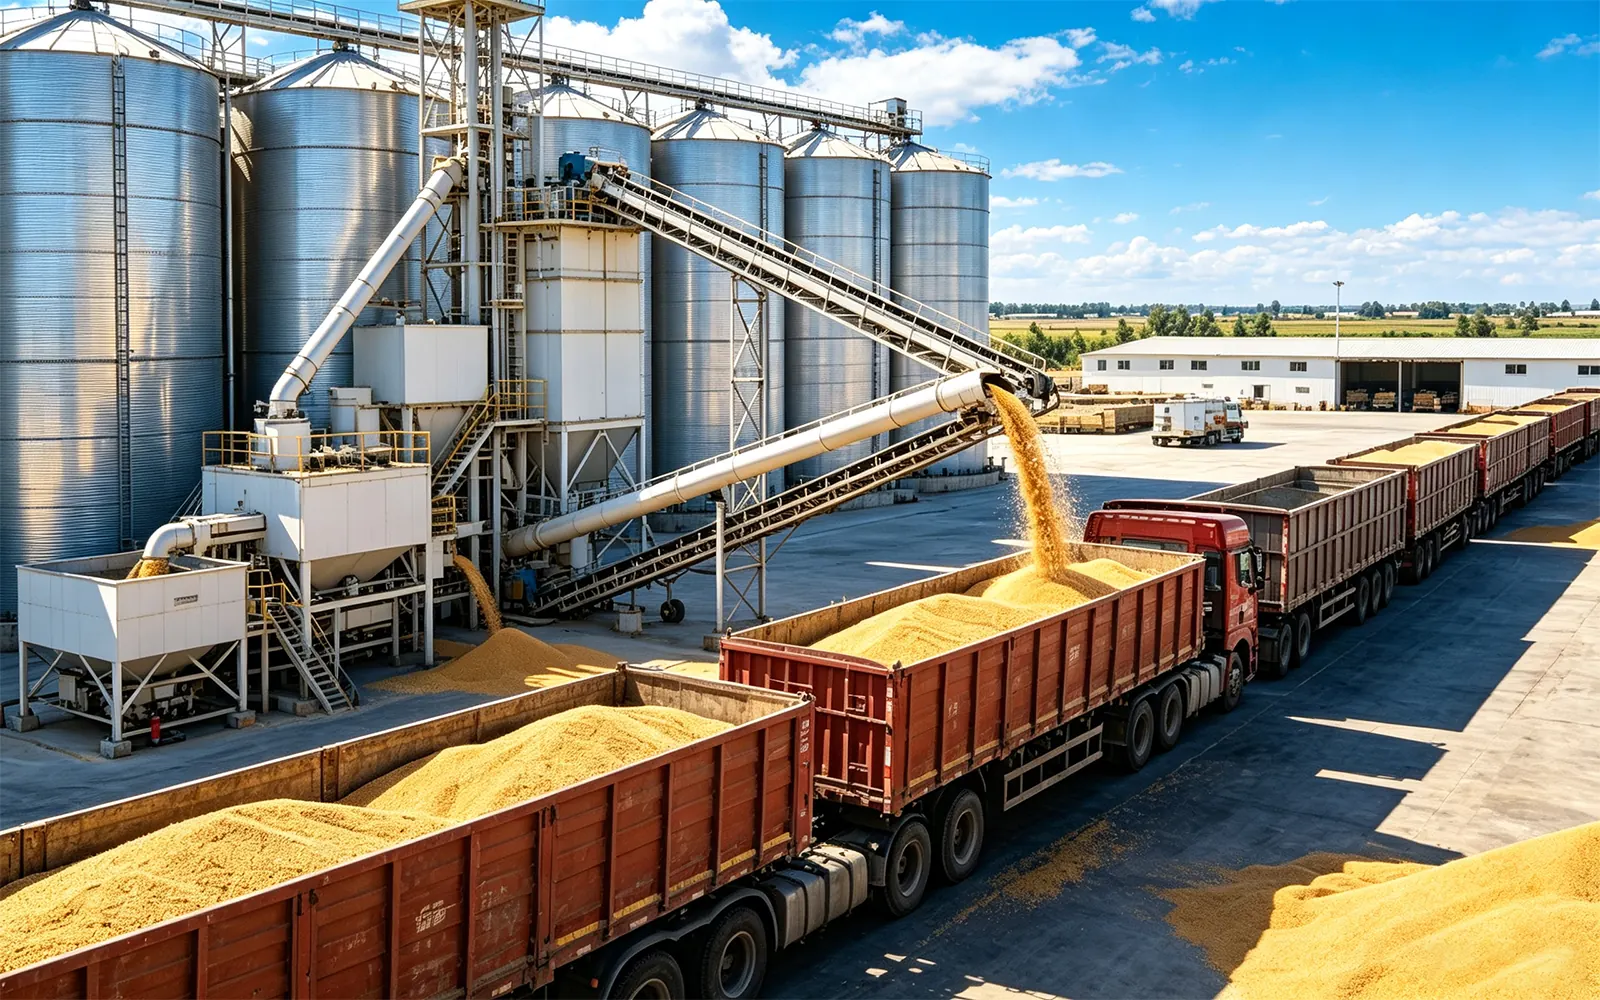
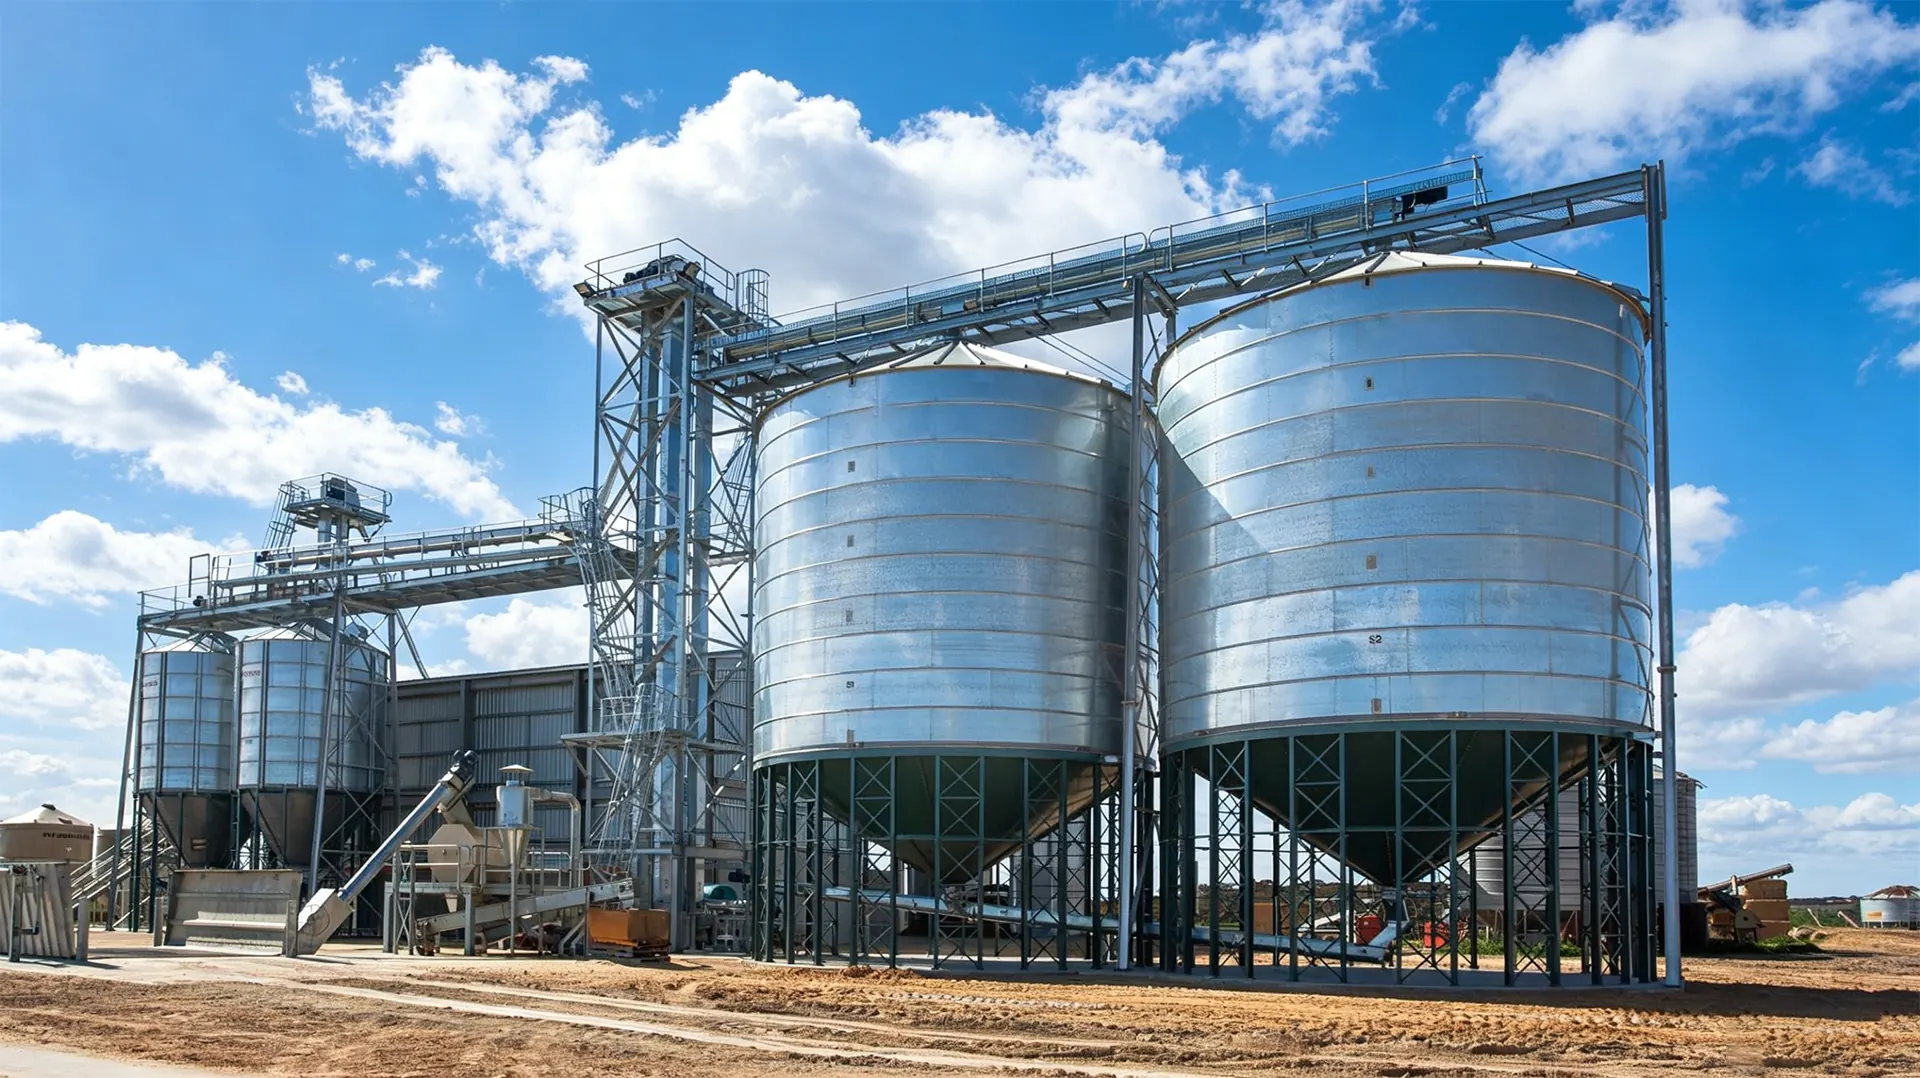
For operators coming from agricultural bulk storage, the good news is that the hardware is familiar. Bolted steel flat-bottom silos, chain and belt conveyors, reclaim tunnels with vibrating feeders, and enclosed load-out systems are proven in both industries. The engineering discipline that changes is the specification of materials, coatings, and drainage.
It is worth framing the economics early, because they are frequently underestimated at feasibility stage. On a typical 30,000 to 60,000 tonne concentrate storage project, the containment package — subgrade preparation, liner or slab, leak detection, drainage, and leachate handling — commonly represents 20% to 35% of total installed capital cost, and a disproportionate share of the environmental bonding and closure liability. A storage shed that is over-specified on steel structure but under-specified on containment is the classic failure mode: it looks robust, photographs well, and still generates an acid seep within three wet seasons. Conversely, a modest building on an excellent containment platform can operate for twenty years with minimal intervention. The lesson is that capital should be pushed down into the ground, not up into the roof, until the containment design is fully resolved.
There is also a scheduling dimension. Containment elements sit at the bottom of the construction sequence and cannot be retrofitted economically once a stockpile has been built on top of them. That makes them the highest-consequence decisions in the project — and the ones most often deferred in favour of visible, easily justified above-ground equipment.
Know Your Material First: Moisture, Sulfide Content, and Oxidation Behavior in Concentrates
No storage design should proceed without a proper bulk material characterization report. A sieve analysis alone is insufficient. You need moisture content and its variability, bulk density at both loose and consolidated states, angle of repose and angle of surcharge, wall friction angle against the intended liner material, abrasiveness, pH of the material in contact with water, and a sulfide sulfur assay.
| Parameter | Typical Range | Design Consequence |
|---|---|---|
| Bulk density (loose) | 1.6 – 2.2 t/m³ | Sets pile surcharge, feeder and conveyor capacity, silo wall loads |
| Angle of repose | 30° – 40° | Determines stockpile footprint and reclaim dead zones |
| Moisture content (filter cake) | 6% – 12% | Controls dust generation, freezing risk, TML compliance for shipment |
| Runoff pH | 2.5 – 5.0 | Drives liner type, concrete mix design, coating selection |
| Sulfide sulfur | 25% – 35% (Cu conc.) | Governs self-heating potential, SO₂ generation, fire risk |
| Chloride content | <100 – 1,000+ ppm | Pitting corrosion risk on stainless and coated steel |
Moisture Content and the Transportable Moisture Limit
Moisture is the single most consequential variable. Below roughly