Choosing between a container silo and a panelized silo is one of the few grain storage decisions that affects your freight invoice, your foundation design, your assembly crew, and your maintenance budget for the next two decades. This Purchase High-Quality Steel Silo: An Engineer's Guide breaks down the engineering, the logistics math, and the total cost of ownership so you can specify the right system the first time.
Key takeaway: Container Different Types of Silos Used in Cement, Mining & Agr... win on speed, mobility, and low-volume economics — typically 8 to 25 tonnes per unit. Panelized silos win on scale, aeration control, and cost per tonne above roughly 100 tonnes, where freight density and seam engineering stop being constraints and start being advantages. The crossover point for most buyers sits between 150 and 300 tonnes of total on-site capacity.

What Is a Container Silo vs a Panelized Silo? Clearing Up Terminology Before You Buy
The terminology in this market is genuinely confusing, and a surprising number of procurement mistakes trace back to a simple misread of a spec sheet. Let's define both Dry Method Cement Rotary Kiln Systems in Modern Cement Pl... precisely.
A container silo — sometimes called a flat-pack silo or a modular bin — is a factory-assembled or factory-fixtured structure built around a rigid steel . The is typically a welded or heavily bolted skeleton of square or rectangular tube, and the grain-retaining surface is formed by relatively small corrugated or flat steel sheets that bolt onto that . The defining characteristic is the : it carries the structural load, and the skin is largely a containment membrane. Units are designed to fit inside or on top of standard ISO shipping footprints, which is where the name comes from.
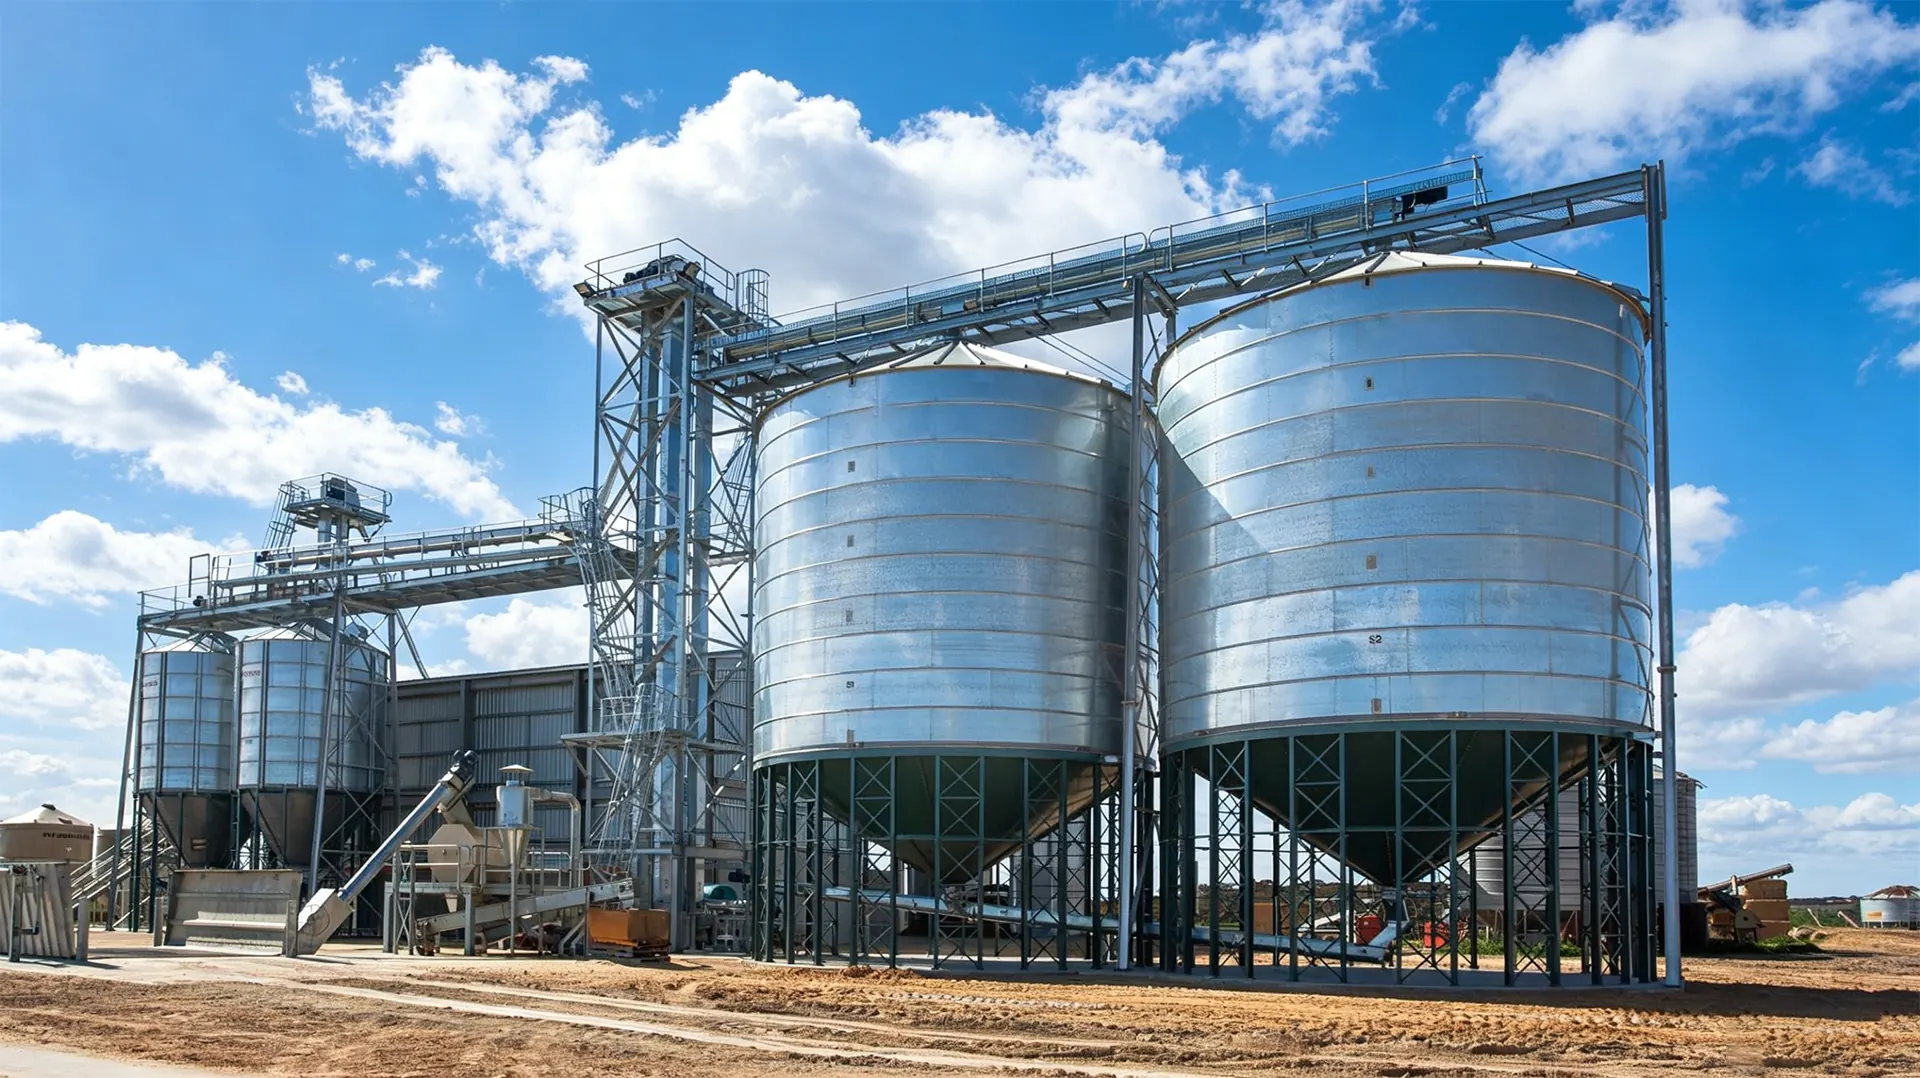
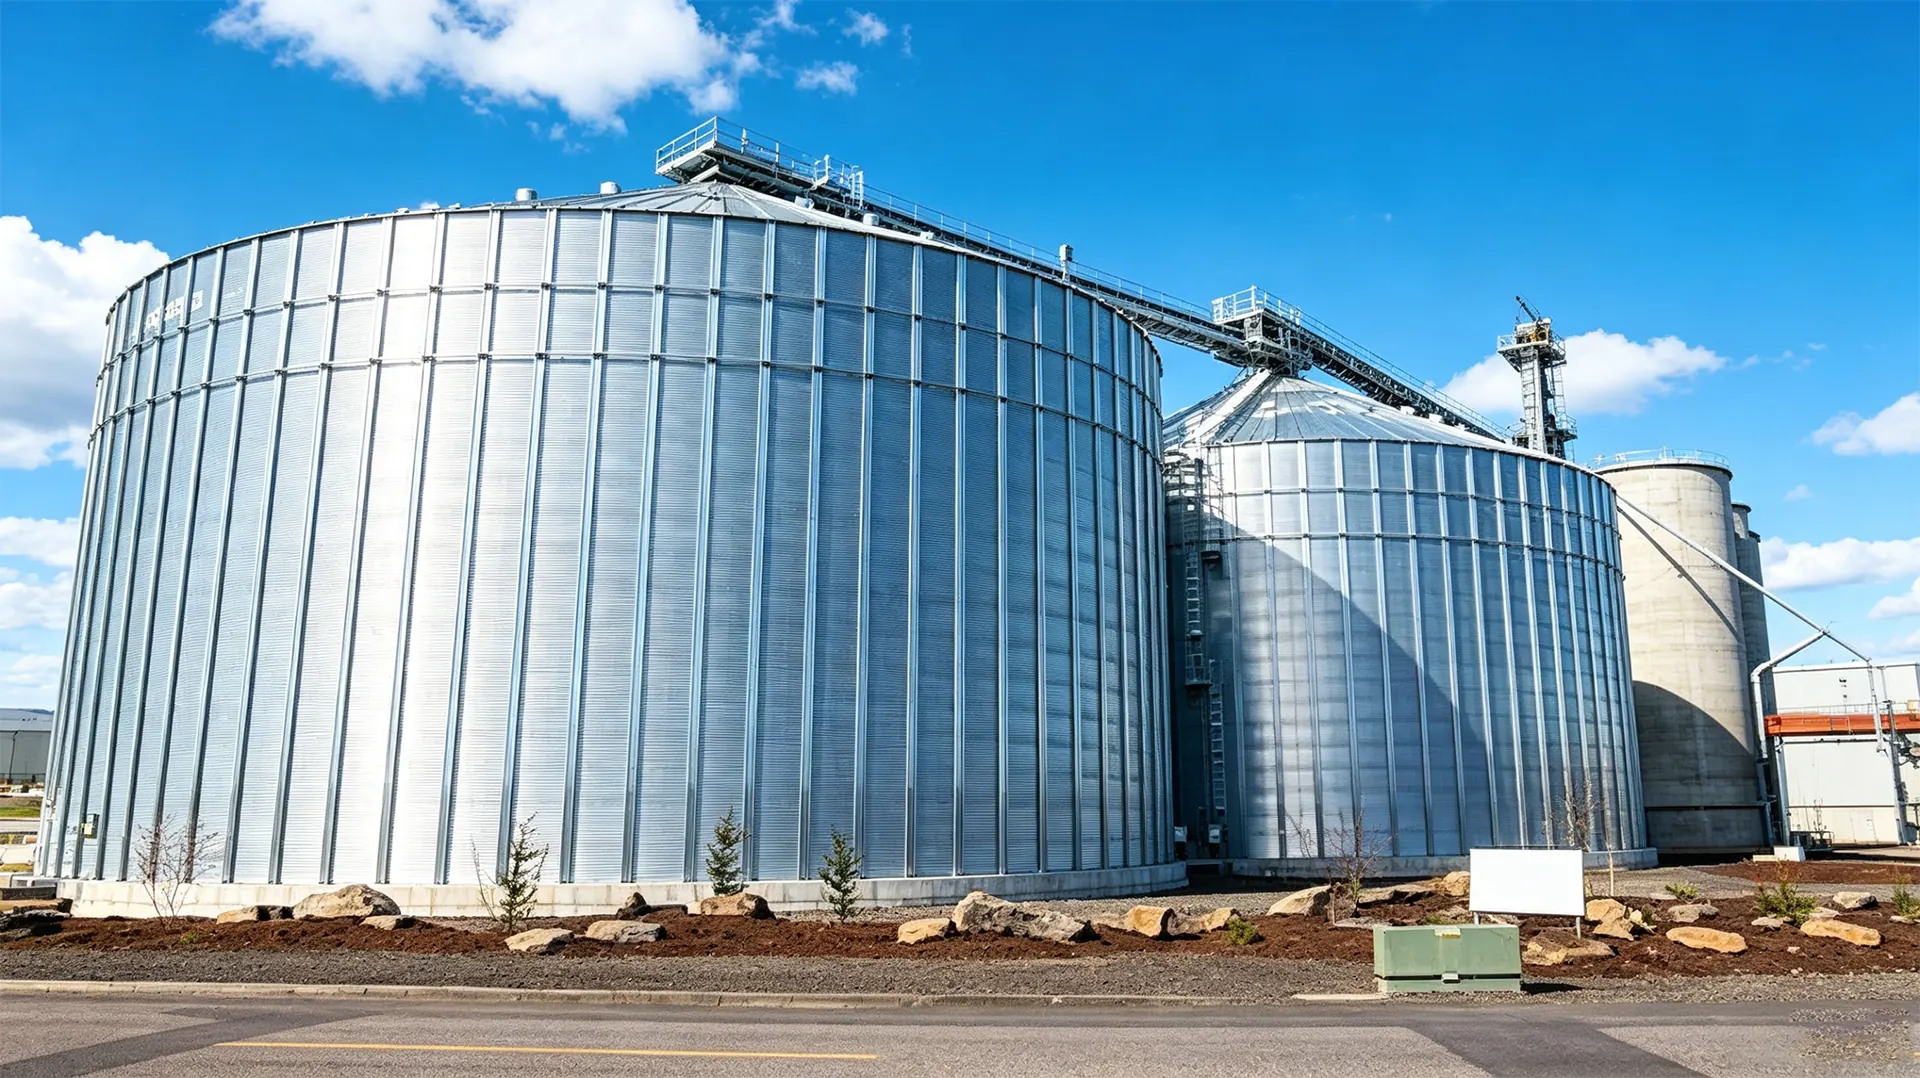
A panelized silo — the conventional bolted grain bin most operators picture — is a self-supporting shell. Corrugated steel panels, usually 1.0 to 4.0 mm thick and roughly 1 to 1.2 metres wide, are bolted together in horizontal rings and vertical courses. The wall itself carries the hoop tension generated by the grain mass. There is no internal skeleton; the shell is the structure.
That single distinction — -supported versus shell-supported — cascades into everything else: freight cost, assembly labour, foundation loads, aeration design, and how the silo behaves when you load it to 100 percent capacity in a coastal wind zone.
How Each System Is Engineered: Flat-Pack Frames, Corrugated Panels, and Bolted Seams Explained
Container silo engineering: the does the work
In a container silo, the vertical load path runs from the roof, through the corner posts and intermediate stiffeners, down to the base and into the foundation. Because the is pre-jigged at the factory, tolerances are tight and the panels are small — often 300 to 600 mm wide. This is a genuine advantage: small panels are light enough for two people to handle without a crane, and the bolted connections are short and numerous, which distributes stress evenly.
The trade-off is redundancy. Every stiffener and every intermediate member is a potential moisture trap, a place where condensation can collect, and a location where grain fines and dust accumulate during loading. Good container silo designs manage this with continuous gaskets and sealed profiles; cheaper ones do not, and the failure shows up three seasons later as caked grain against a corroded stiffener.
Panelized silo engineering: the shell carries the hoop stress
A panelized grain silo is a thin-shell pressure vessel operating in a non-uniform load case. Grain exerts lateral pressure that increases with depth, so wall thickness is stepped — heavier panels near the base, lighter panels toward the top. Hoop tension at the base of a 10-metre-diameter silo filled with 8 metres of wheat is substantial, which is why high-tensile bolts (grade 8.8 or better) and controlled torque values matter far more than most buyers realise.
Corrugation geometry is not cosmetic. It adds effective stiffness to a very thin plate, allowing a 2.5 mm panel to behave like a much thicker flat sheet in hoop tension. Vertical corrugations also create a natural vertical air channel between the panel and the grain mass, which is directly relevant to aeration performance later in this article.
Seam count: the hidden variable
Here is a number worth remembering. A 500-tonne panelized silo might have 180 to 260 bolted panel seams. A container silo of comparable capacity built from small modular panels can exceed 700. Every seam is a bolt, a gasket, a torque value, and a future inspection point. This is not automatically a defect — but it is a maintenance liability that scales with seam count, and it is the single most under-quoted factor in container silo lifecycle costing.
Capacity, Footprint, and Configuration Options
Both systems span a wide range, but their sweet spots are very different.
| Parameter | Container Silo | Panelized Silo |
|---|---|---|
| Typical capacity range | 8 – 150 tonnes per unit | 20 – 5,000+ tonnes per unit |
| Practical sweet spot | 10 – 40 tonnes | 150 – 2,000 tonnes |
| Diameter / footprint | Fixed modular footprint, often 2.2–3.5 m | 3 m to 30 m+ diameter, fully scalable |
| Hopper bottom | Common and factory-fitted | Available, usually as a separate cone section |
| Flat bottom | Available with sweep auger | Standard for large capacity |
| Expansion capability | Add discrete units (modular) | Ring/course addition on some models only |
| Relocation | Fully relocatable, designed for it | Difficult and rarely economical |
Hopper bottom versus flat bottom
Hopper-bottom configurations are where container silos genuinely shine. A 45-degree or 60-degree cone discharging into a 200 mm outlet gives you mass-flow behaviour, minimal residual grain, and clean changeover between varieties — critical for seed producers and specialty crop operations. Panelized silos can be supplied with hopper bottoms, but the cone adds significant height and cost, and above roughly 300 tonnes the cone geometry becomes impractical to fabricate and ship.
Flat-bottom panelized silos with sweep augers dominate at commercial scale because they maximise storage volume per square metre of expensive concrete. If your site has a fixed footprint and you need maximum tonnes, flat-bottom panelized is almost always the answer.
Delivered Cost Per Tonne: The Freight Density and Shipping Container Math Most Suppliers Won't Show You
Equipment price is not the number that matters. Delivered cost per tonne is, and freight density drives it.
Panelized silo components are engineered to nest. Corrugated panels stack almost perfectly flat, roof sheets stack, and stiffeners bundle. A 40-foot high-cube container can carry enough panelized components for a substantial silo because the load is essentially two-dimensional. Freight density for panelized components typically lands in the 180–320 kg per cubic metre range when properly packed.
Container silos ship as three-dimensional frames. A pre-welded does not nest. Unless the unit is specifically designed for knock-down shipment, you are paying to move air. Freight density for -based modular units commonly falls between 60 and 140 kg per cubic metre — meaning you may need two to four times the container volume to move the same steel mass.
A worked example
Take a 100-tonne requirement. Option A: five 20-tonne container silos. Option B: one 100-tonne panelized silo.
- Container silos: approximately 5 × 12 m³ of shipped volume = 60 m³, plus void space, realistically 3–4 containers.
- Panelized silo: approximately 18–22 m³ of nested components, comfortably 1 container with room for augers and accessories.
At a typical international container rate, that freight delta alone can swing delivered cost per tonne by 15 to 35 percent — before you account for the extra unloading labour, the extra site handling, and the extra bolted joints. For domestic buyers within 500 km of the factory, truck freight narrows the gap considerably, and the container silo's assembly-speed advantage can recover the difference.
Rule of thumb: If your supplier quotes FOB or ex-works prices without a delivered-volume calculation, you are not comparing silos — you are comparing catalogue numbers. Always request a landed cost per tonne, including freight volume, port handling, and inland transport.
Assembly Time, Labor, and Crane Costs: Realistic Installation Timelines
Assembly is where container silos earn their reputation, and where panelized silos demand respect for process.
A 20-tonne container silo with a pre-assembled and pre-punched panels can typically be erected by a three-person crew with a telehandler in one to two days, including roof and ladder. No crane is usually required for units under about 6 metres to eaves. That is a genuine advantage for remote sites, island installations, and operations where mobilising a crane costs more than the silo.
A panelized silo is a different project. A 500-tonne flat-bottom bin with aeration floor, sweep auger, sidewall ladder, roof vents, and a catwalk realistically takes 5 to 12 working days with a 4–6 person crew and a crane on site for roof ring and upper course placement. Larger commercial bins with 20-metre diameters routinely run three to five weeks.
| System | Typical crew | Crane required | Erection time (per unit) |
|---|---|---|---|
| 20 t container silo | 2–3 | Usually no (telehandler) | 1–2 days |
| 100 t container silo cluster | 3–4 | Sometimes | 4–8 days |
| 100 t panelized silo | 4–5 | Yes, 1–2 days | 4–7 days |
| 500 t panelized silo | 4–6 | Yes, 3–5 days | 8–14 days |
| 2,000 t panelized silo | 6–8 | Yes, 2–3 weeks | 20–35 days |
The costs nobody quotes
Two line items consistently surprise buyers. First, anchor bolt setting and foundation cure time — a panelized silo foundation needs 7 to 28 days of cure before loading, which can delay commissioning even when steel erection is fast. Second, touch-up painting and torque verification: every bolted connection must be torque-checked and every scratched galvanised surface re-coated. On a 700-seam container silo, that is a full day of one technician's time that simply does not exist on a 200-seam panelized bin.
Seams, Gaskets, and Bolts: How Panel Count Quietly Determines Aeration, Fumigation, and Grain Quality Outcomes
This is the section that separates buyers who have run silos for twenty years from buyers who have run them for two.
Every bolted seam is a potential leak path. In aeration, leaks mean air short-circuits to the path of least resistance instead of travelling uniformly through the grain mass. The result is uneven moisture, hot spots, and mould risk in exactly the zones you cannot see. In fumigation, leaks mean phosphine or sulfuryl fluoride escapes before reaching lethal concentration at the top of the grain column — and the operator, believing the job is done, stores infested grain.
Seam density and air-tightness
A panelized silo with 200 seams and continuous pre-formed butyl gaskets on every lap can achieve a pressure-hold specification suitable for sealed fumigation, typically expressed as the time to decay from 500 Pa to 250 Pa. Well-built commercial bins routinely exceed 5 minutes; premium sealed bins reach 10 to 15 minutes.
A container silo with 700 seams must rely on the same gasket discipline multiplied